How the Pneumatic System Supports Reliable Block Plant Automation
The main forming movements of an automatic concrete block machine are commonly driven by hydraulic, electric or servo systems. This can make compressed air appear secondary. In a complete production line, however, pneumatic cylinders and valves may operate aggregate gates, mixer discharge gates, diverters, cleaning nozzles, positioning stops, grippers or strapping equipment. If air pressure falls or condensate reaches a valve, one small actuator can interrupt the sequence of the entire line.
A reliable pneumatic system depends on more than purchasing a compressor with a large motor. The plant needs sufficient flow at the required pressure, effective water removal, correctly sized pipes, suitable air treatment and a maintenance routine. This article explains how those elements affect production rhythm and how operators can diagnose common problems without confusing them with electrical or hydraulic faults.
Where Compressed Air Is Used
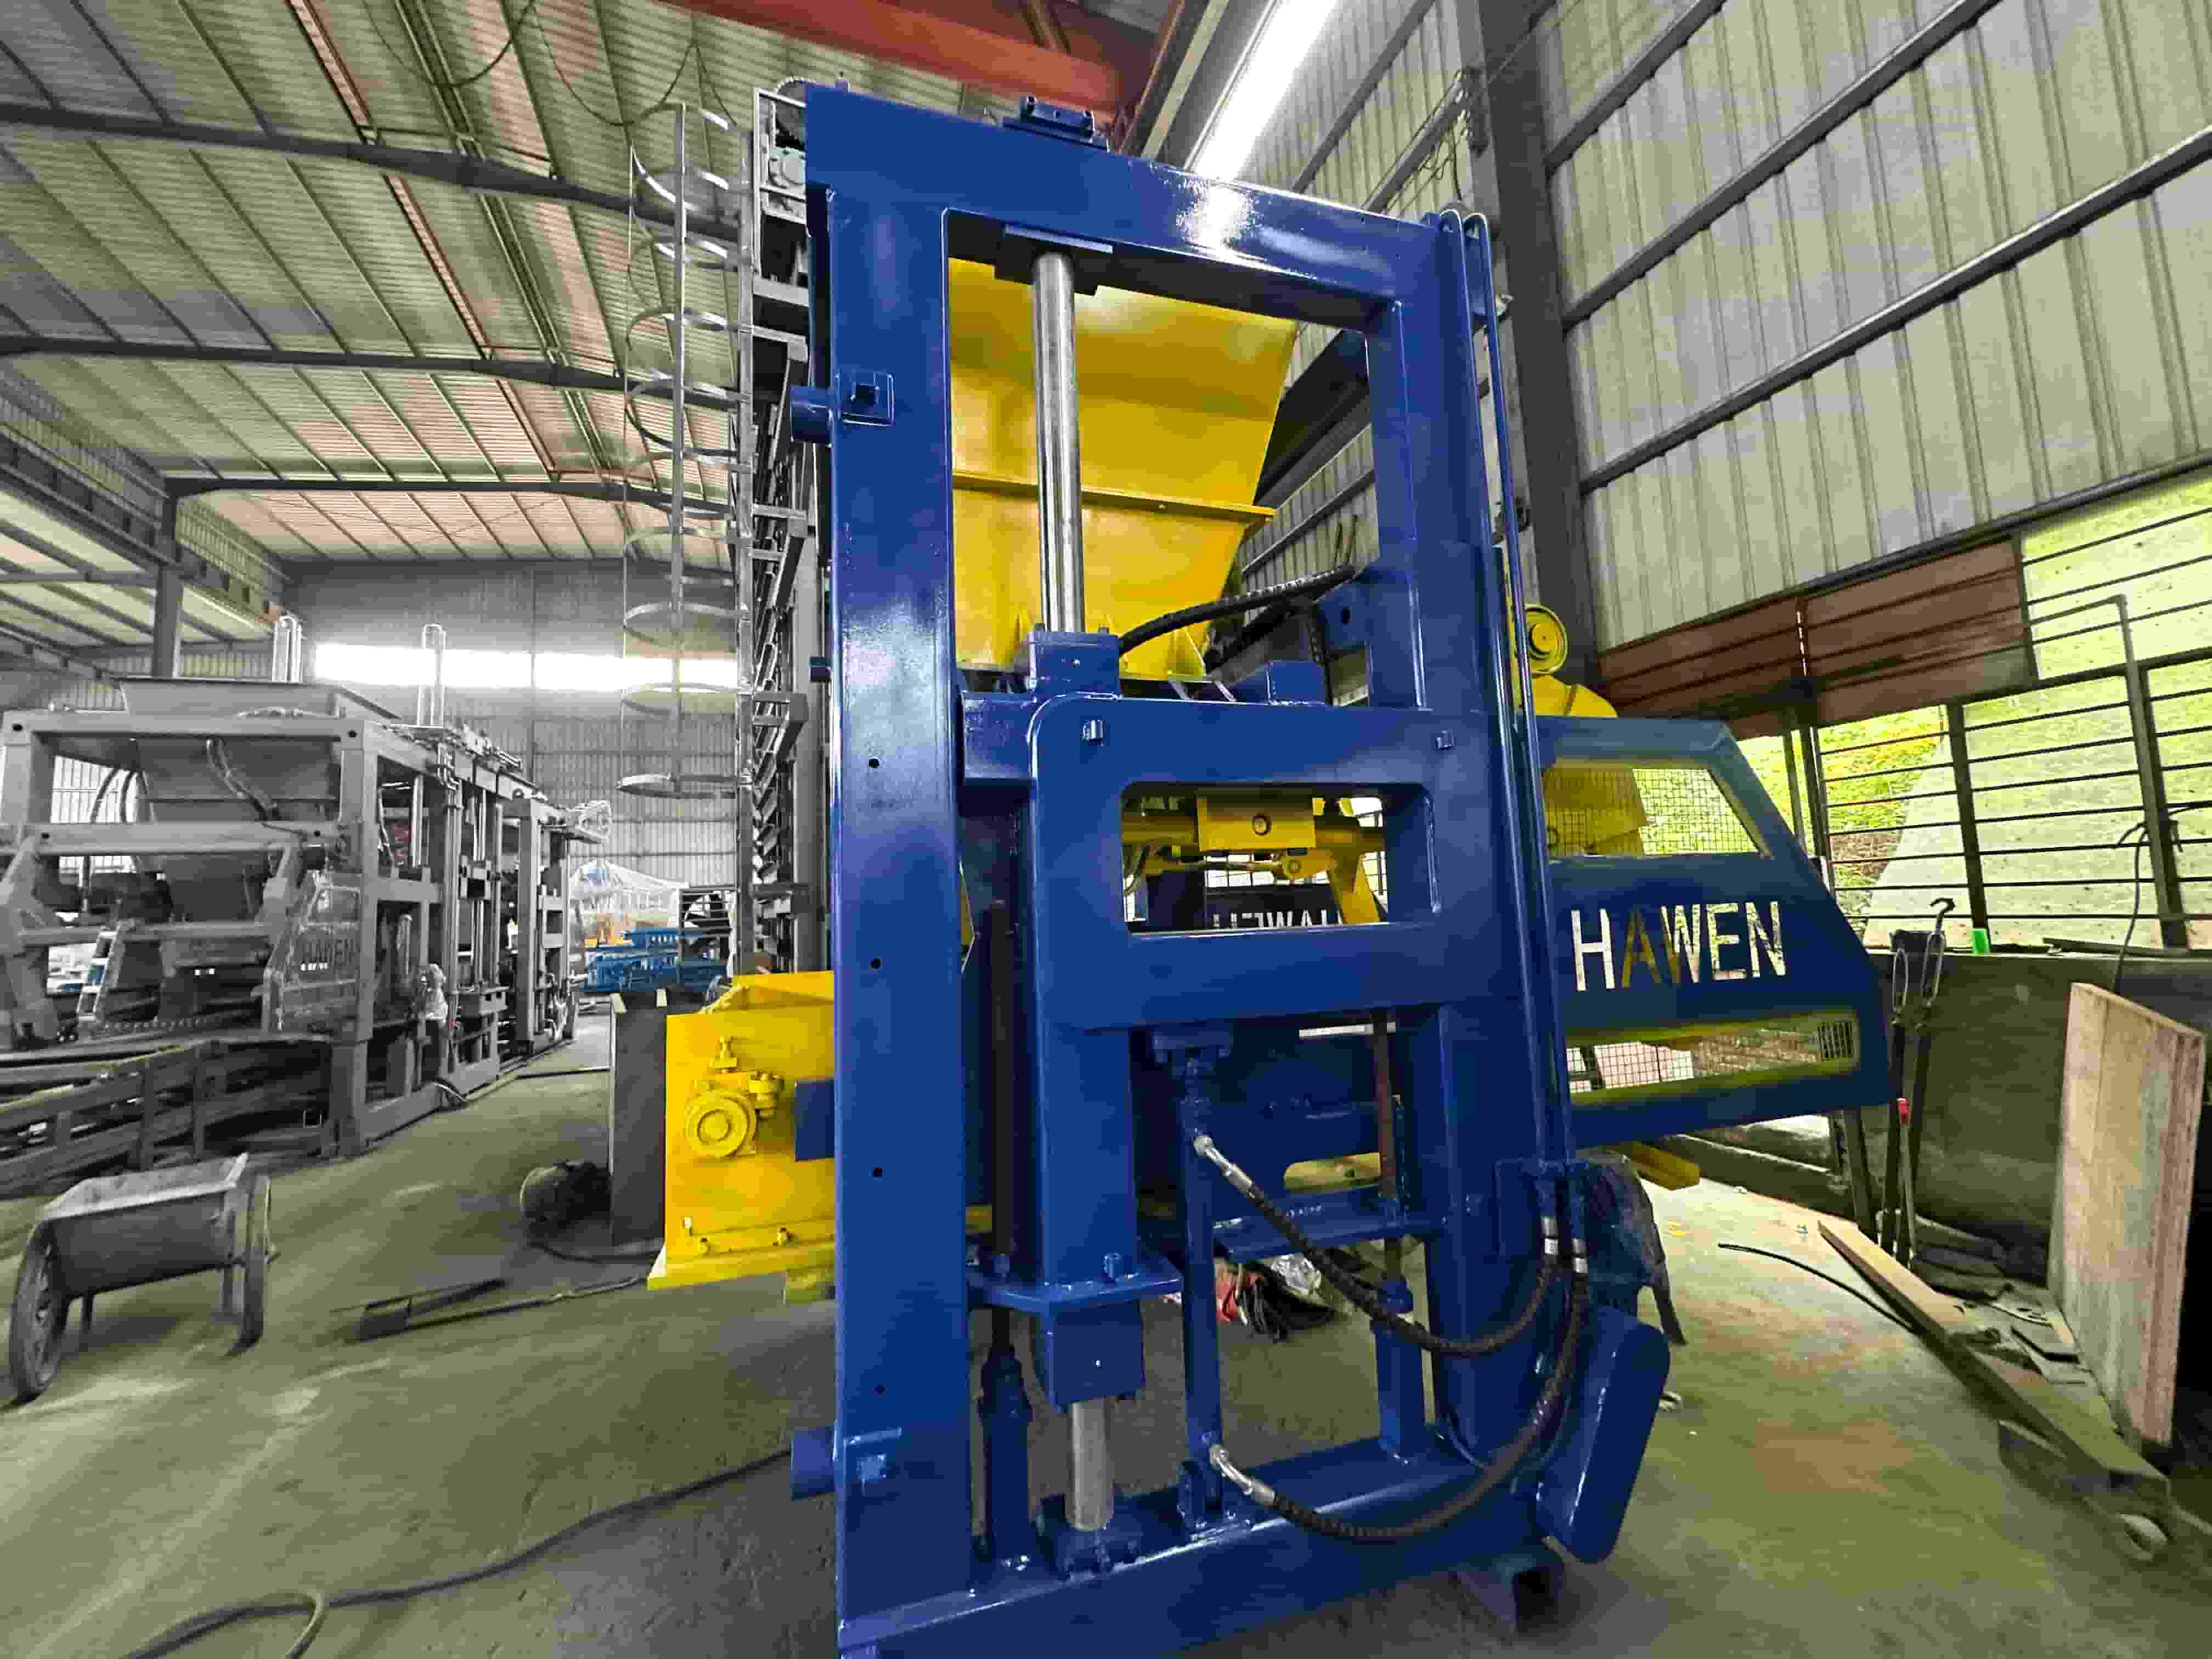
The exact uses depend on line configuration. In batching equipment, pneumatic cylinders may open and close aggregate discharge gates. At the mixer, air may operate a discharge door or auxiliary diverter. On the forming and conveying sections, it may actuate stops, clamps, alignment devices or cleaning nozzles. Downstream equipment may use compressed air for gripping support, strapping and package handling.
Each function has a different demand pattern. A small stop cylinder uses little air but may move every production cycle. A large gate cylinder consumes more air during short opening and closing events. Air cleaning creates a high continuous flow while its nozzle is open. When several actions occur together, their combined peak demand can be much higher than the average shown over one minute.
The control system expects each actuator to complete within a defined time. A position sensor then permits the next step. If a gate moves slowly because of low pressure, the PLC may wait, alarm or proceed with an incomplete material discharge depending on the logic. Thus, a pneumatic issue can appear as irregular batching, long cycle time or a sensor fault. Understanding the sequence is essential for diagnosis.
A complete automatic block machine line should therefore identify every compressed-air consumer on its utility list. The list should state required pressure, estimated normal and peak consumption, air quality and whether loss of air leaves the actuator in a safe position.
Pressure, Flow and Air Quality
Pressure and flow are related but not interchangeable. A receiver may show adequate pressure while the system is idle, then pressure at a remote valve can fall sharply when several cylinders move. This usually indicates insufficient compressor capacity, a restriction, excessive leakage, undersized piping or inadequate storage close to a high-demand section. Measure pressure during the actual operating event and at the point of use.
Higher pressure is not a general cure. It increases energy consumption, leakage and actuator force, and it can exceed component ratings. Use the machine supplier's specified pressure and adjust local regulators for each function. If an actuator only works after the regulator is raised above its normal setting, investigate load, friction, valve flow, tubing and cylinder condition.
Ambient air contains water vapor. Compression raises the concentration of moisture, and cooling in the receiver or pipes causes condensate. Water can corrode components, wash lubricant from surfaces, make valves stick and freeze in cold conditions. A compressor installation normally needs a receiver, drains and suitable drying or water separation based on the local climate and required air quality.
Dust and oil also matter. Block plants generate cement and aggregate dust that can enter the compressor intake or open tubing during maintenance. Filters should match the sensitivity of downstream valves and instruments. Where an oil-injected compressor is used, the treatment system must control oil carryover to the level required by the equipment. Some components require lubricated air and others do not; follow the supplier's specification rather than adding an oiler automatically.
Main Pneumatic Components
The compressor supplies air, while the receiver stores air and reduces rapid load fluctuations. A dryer or separator removes moisture, filters remove particles and aerosols, and regulators set working pressure. Distribution pipes carry air to local valve manifolds. Solenoid valves direct flow, cylinders convert it into linear movement, and flow controls set movement speed. Pressure switches and position sensors provide information to the PLC.
Each component can affect timing. A blocked filter creates pressure drop. A regulator with insufficient flow capacity may hold the set pressure at rest but restrict a large cylinder. A solenoid valve can receive the electrical command yet fail mechanically because its spool is contaminated. A worn cylinder seal can leak internally, reducing force without an obvious external hiss.
Flow controls should be adjusted with care. Excessive restriction makes an actuator slow and can cause a timeout; unrestricted movement can slam a gate or stop, damaging mounts and creating inconsistent material flow. After setting the correct speed, lock or record the adjustment. If operators repeatedly change a flow control to keep production running, find the underlying pressure or mechanical problem.
Flexible tubing near moving equipment should have sufficient bend radius and protection from abrasion, heat and sharp edges. Push-in fittings must use compatible tubing and a clean square cut. Long unsupported tubes can vibrate and fatigue. Labeling valve outputs and tubes shortens troubleshooting time when a line includes several similar actuators.
How Pneumatic Faults Affect the Cycle
At the aggregate batching machine, a slow gate can cause overshoot or incomplete discharge. If the gate closes late, extra material falls after the target is reached. If it does not open fully, material flow becomes irregular and the batch takes longer. The resulting mix variation may later be blamed on the mixer or block machine even though it began at a pneumatic actuator.
A mixer discharge gate that opens slowly extends the transfer time and can leave residual material inside. A gate that does not seal can allow material to leak onto a conveyor before the intended discharge. Both conditions disrupt the programmed sequence. Before changing PLC delays, confirm that the cylinder receives stable pressure and the gate moves freely without material buildup. The selected concrete mixer configuration should be included when the plant prepares its compressed-air consumer list.
Positioning stops and clamps require repeatability. If a pallet or product layer stops a few millimeters differently from one cycle to the next, downstream gripping or stacking can become inconsistent. Low pressure may be one cause, but worn guides, a loose sensor bracket or impact damage can create the same symptom. Inspect mechanical and pneumatic conditions together.
Compressed-air cleaning should be controlled because open blowing is a large demand and can spread cement dust. Use appropriately designed nozzles and operate them only for the required duration. A permanently open or broken nozzle can lower pressure throughout the plant and cause unrelated cylinders to slow. It also wastes significant compressor energy.
| Production symptom | Possible pneumatic cause | First checks |
|---|
| Cycle occasionally waits for a gate | Pressure drop, sticky valve or restricted flow | Pressure during motion, filter indicator and valve command |
| Batch weight overshoots | Discharge gate closes too slowly | Cylinder speed, gate friction and control timing |
| Actuator is weak in one direction | Valve restriction, seal leakage or blocked exhaust | Tubing, silencer, manual valve test and cylinder condition |
| Several devices slow together | Plant supply or peak-flow shortage | Receiver pressure, main line pressure and simultaneous demand |
Sizing and Installation Questions
Collect consumption data from every equipment supplier and note which actions overlap. Size the compressor for expected operating demand with a practical allowance for leakage and future equipment, while avoiding prolonged operation outside the compressor's efficient range. The air receiver should support demand changes and stable compressor control. Exact sizing should be completed by a qualified compressed-air supplier using the real duty cycle.
Pipe diameter should limit pressure drop at peak flow. A ring main can improve pressure distribution in larger plants, while short branch lines and local receivers may help high-demand equipment. Slope pipes and provide drain points so condensate does not collect at low sections. Take branch connections in a way that reduces carried water, following the compressed-air designer's practice.
Place the compressor where intake air is reasonably clean and ventilation is adequate. Compressor heat must be removed, especially in a hot climate. At the same time, avoid extremely long pipe runs between compressor and production line. Provide access around filters, dryer, receiver drains and service components. A machine hidden behind stored pallets will not receive regular maintenance.
Electrical integration also matters. The compressor, dryer and automatic drains may need status signals or alarms. A low-pressure switch can stop a sequence before an actuator becomes unpredictable. The PLC should give a useful message that identifies the affected air zone or action. A generic “cycle timeout” forces operators to search across many systems.
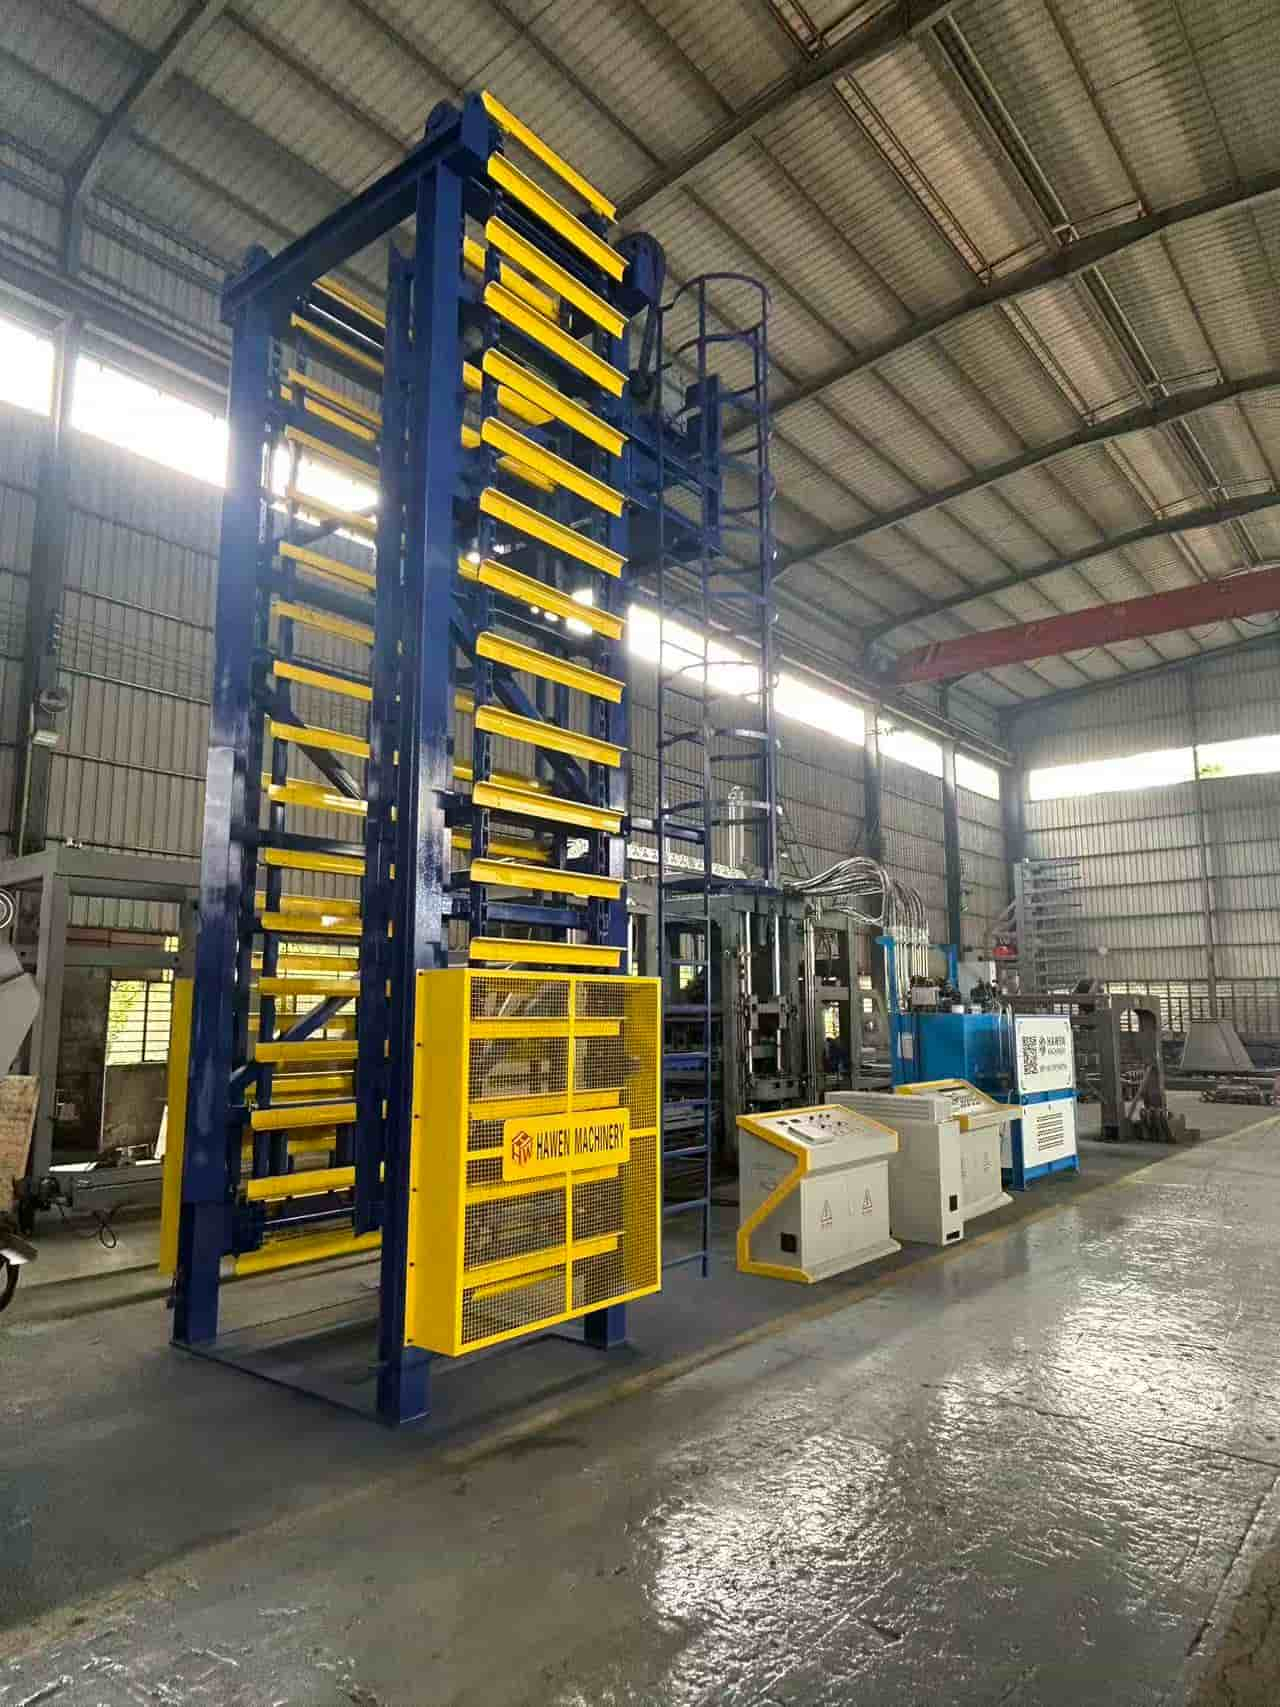
For a downstream automatic cuber system, confirm whether gripping is hydraulic, electric, pneumatic or a combination. Do not assume that one utility description covers every version. Obtain a final interface schedule showing electrical power, hydraulic requirements and compressed-air requirements for the purchased configuration.
Inspection and Maintenance
Drain condensate at the receiver, filters and low points according to site conditions. Automatic drains should be tested because a blocked drain can appear normal from outside. Inspect filter indicators and replace elements based on pressure drop and the manufacturer's interval. Service dryers so that air quality remains stable through humid seasons.
Leak inspection offers a direct return. Listen during shutdown, use an approved leak-detection method and tag each leak for repair. Check fittings, tube damage, valve exhausts and cylinder rods. A large number of small leaks can keep the compressor loaded during production breaks and reduce pressure when the line reaches peak demand.
Keep cylinder rods clean and inspect mountings, pins and alignment. A cylinder should not compensate for a bent gate or misaligned linkage. Side loading shortens seal and bearing life. Where cement dust accumulates, improve guarding or cleaning methods rather than repeatedly replacing contaminated components.
Record regulator settings, normal pressure during a cycle and typical actuator times. This baseline helps distinguish a gradual restriction from a sudden mechanical jam. Keep critical solenoid coils, valve service parts, tubing and fittings appropriate to the installed equipment. Verify part specifications before substitution, including voltage, port size, flow capacity and environmental rating.
Practical Troubleshooting
Start with the sequence. Identify the actuator that failed to complete and determine whether the PLC issued its command. If there is no command, inspect interlocks and sensors. If there is a command, check the solenoid indication and voltage using qualified personnel. Then verify pressure at the valve and cylinder while the movement is attempted.
Separate supply problems from local problems. If several actuators slow simultaneously, inspect compressor, receiver, dryer, main filter and common piping. If only one actuator is affected, inspect its regulator, valve, flow controls, tubes, exhaust silencer and mechanical load. Swapping adjustments without this distinction can disturb devices that were working correctly.
Use the valve's approved manual override only under the equipment's safe maintenance procedure. A successful manual movement suggests that the pneumatic path and mechanism may be functional, while the electrical command or interlock needs review. An unsuccessful movement points toward pressure, valve, cylinder or mechanical resistance. Release stored air before disconnecting any tube or component.
After repair, run multiple cycles under normal load and monitor pressure at the point of use. Confirm that the original timing and product result are restored. Update the maintenance record with the failed part and cause. Repeated valve contamination indicates an air-quality problem; repeated cylinder damage indicates alignment or load problems. Replacing the same part without correcting the cause only resets the failure clock.
FAQ
Why does the pressure gauge look normal while a cylinder moves slowly? The gauge may show static pressure. A restriction or insufficient peak flow can cause pressure to fall only during movement, so measure near the actuator while it operates.
Can the compressor pressure simply be increased? Use the specified pressure. Increasing it raises energy use and forces and may hide a restriction, leak or mechanical problem.
Why is there water in pneumatic tubing? Water vapor condenses as compressed air cools. Inspect drains, separators, dryer performance, pipe slope and local climate conditions.
Can a pneumatic fault change block quality? Yes. If it changes aggregate discharge, mixer emptying, pallet positioning or the production cycle, it can indirectly affect material proportions and forming consistency.
How often should air leaks be checked? Set a regular interval based on operating hours and dust conditions, and inspect whenever compressor run time or pressure drop increases unexpectedly.
Conclusion
Compressed air coordinates many small actions that keep a block line moving. Stable pressure at peak demand, clean and dry air, correctly sized components and disciplined leak maintenance prevent those actions from becoming production bottlenecks. Treat the pneumatic system as part of process control, and diagnose it through the actual sequence rather than changing machine timing at the first alarm.


 Tel: +86-13905968794
 Email: export@hwmachines.com
 MP/WhatsApp: +86-13905968794
 Manufacturer Address:Nanan,Quanzhou City,Fujian Province,China